
Call us now :08045814986
 Send Inquiry

 Send Inquiry
Polysorbate 80 Tween 80
Price 145 INR/ Kilograms
MOQ : 100 Kilograms
Polysorbate 80 Tween 80 Specification
- Smell
- Odorless or mild odor
- Taste
- Slightly bitter
- Appearance
- Viscous liquid
- Shelf Life
- 2 years
- Heavy Metal (%)
- < 0.001%
- Molecular Formula
- C64H124O26
- Physical Form
- Liquid
- Assay
- Minimum 99%
- Melting Point
- -5C to 0C
- Water Solubility
- Soluble
- Solubility Tests
- Soluble in water, insoluble in oils
- Boiling point
- Not applicable (decomposes)
- CAS No
- 9005-65-6
- Other Names
- Tween 80, Polyoxyethylene (20) sorbitan monooleate
- Type
- Non-ionic surfactant
- Color
- Light yellow to amber
- Purity
- 99%
- Application
- Pharmaceutical, food, cosmetics
- Storage
- Cool, dry place
- Packaging Type
- HDPE Drum
- Viscosity
- High
- Imported available
- Yes
- Non-flammable
- Yes
- Industrial use
- Common
- Food grade
- Available
- Prescription/Non prescription
- Non prescription
- Packaging Size
- 220 Kg
- Transport
- Bulk drum
- Form
- LIQUID
- Container color
- Blue
- Emulsifier category
- Accepted
- Reagent grade
- Available
- Pharma grade
- Available
Polysorbate 80 Tween 80 Trade Information
- Minimum Order Quantity
- 100 Kilograms
- Supply Ability
- 5000 Kilograms Per Month
- Delivery Time
- 7 Days
About Polysorbate 80 Tween 80
Discover Polysorbate 80 (Tween 80), a top-tier, non-ionic surfactant, renowned for its flawless emulsifying power in pharmaceutical, food, and cosmetic formulations. This first-string, highly viscous liquid offers an enlightened choice for manufacturers, suppliers, and traders seeking high purity (99%) and accepted food, pharma, and reagent grade quality. Available in non-prescription, bulk 220 kg HDPE drums, and imported options, our Polysorbate 80 ensures non-flammable, color-consistent (light yellow to amber), odorless, and safe transport. Purchase with confidence for versatile industrial, manufacturing, and scientific applications.
Wide-Ranging Utility and Standout Features
Polysorbate 80 (Tween 80) is an advanced emulsifier widely adopted across pharmaceuticals, food production, and cosmetics. Its high viscosity and non-ionic nature guarantee seamless blending and stability in products requiring both oil and water components. Its flawless solubility in water, nearly imperceptible odor, and minimal heavy metals presence make it a first-string choice for applications where purity and functionality are essential. For general and specialized use, it brings exceptional efficacy and reliability.
Exceptional Supply Chain and Packaging Solutions
Our order processing system prioritizes swift handover and quick dispatch from multiple FOB ports within India, ensuring minimal downtime for your supply chain. Polysorbate 80 comes in sturdy blue HDPE drums, with a generous 220 kg packaging size for efficient bulk transport. Imported and domestic stocks are available to meet diverse demand, making us a top supplier for manufacturers, traders, wholesalers, and end-users seeking consistent quality and rapid fulfillment.
FAQ's of Polysorbate 80 Tween 80:
Q: How is Polysorbate 80 (Tween 80) typically used in industry?
A: Polysorbate 80 serves as a powerful emulsifying agent in pharmaceutical, food, and cosmetic formulations, stabilizing mixtures containing oil and water.Q: What are the key benefits of using Polysorbate 80 in manufacturing?
A: Benefits include flawless solubility in water, a high purity level (minimum 99%), and its non-flammable, safe-to-handle nature, making it ideal for sensitive applications.Q: When should I choose food, pharma, or reagent grade Polysorbate 80?
A: The grade should match your application: food grade for consumables, pharma grade for medicines, and reagent grade for laboratory or analytical processes.Q: Where is Polysorbate 80 supplied from and in what packaging?
A: It is supplied from multiple FOB ports across India, available in robust blue HDPE drums of 220 kg, suitable for bulk orders.Q: What is the process for order processing and delivery?
A: Once an order is placed, processing begins immediately with priority handover and quick dispatch to ensure timely delivery to your location.Q: Is Polysorbate 80 safe for use in food and pharmaceuticals?
A: Yes, with a purity of 99%, minimal heavy metal content, and approval for food and pharma grade applications, it meets the highest safety standards.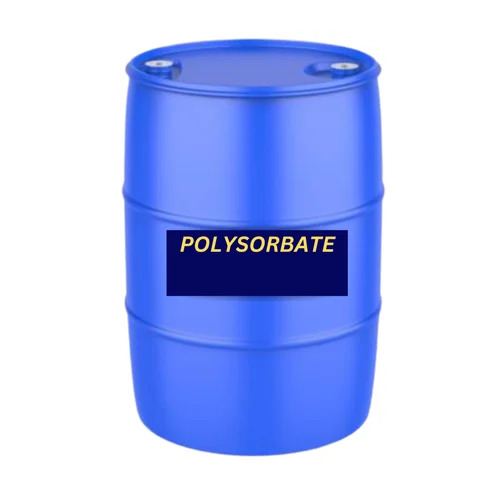
Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Food Additive Category
Softemul 165 FLAKES
Price 118 INR / Kilograms
Minimum Order Quantity : 100 Kilograms
Shelf Life : 2 Years
Purity : >99%
Taste : Other ,
Storage : Other, Cool, Dry Place
Sodium Saccharin Powder
Price 99 INR / Kilograms
Minimum Order Quantity : 100 Kilograms
Shelf Life : 2 years
Purity : 99% Min
Taste : Sweet
Storage : Other, Cool, dry place
Citric Acid Monohydrate
Price 80 INR / Kilograms
Minimum Order Quantity : 100 Kilograms
Shelf Life : 2 years
Purity : 99.8%
Taste : Sour
Storage : Other, Cool, dry place
Aspartame Sweetener Powder
Price 956 INR / Kilograms
Minimum Order Quantity : 10 Kilograms
Shelf Life : 2 years
Purity : 98%
Taste : Other , Sweet, clean taste
Storage : Other, Cool, dry place

 Send Inquiry
Our Products
- Calcium Chloride
- Isopropyl Alcohol
- Magnesium Chloride Flakes
- Liquid Triethanolamine
- Butylated Hydroxy Toluene
- Silicone Oils
- Pearl Powder
- Ammonium Chloride
- Acid Thickener
- Melamine Powder And Liquid
- Nonyl Phenol Ethoxylate
- Liquid Glycol Chemical
- Dimethylformamide Liquid
- Alcohol Based Hand Sanitizer
- Paver Block Lacquer Polish
- Polycarboxylate Ether Superplasticizer
- Light Liquid Paraffin Lip Oil
- Sodium Polyacrylate
- Perchloroethylene Chemical
- Pe Waxes
- Gold Nanoparticles
- Acrylamide
- Formalin Liquid
- Methylene Chloride For Pharmaceutical Industry
- Herbal Rat Repellent
- Sulfonated Melamine Formaldehyde
- Liquid Bromine
- Moisture Powders and Moisture Additives
- Vitamin C Injection
- Toluene And Chemical Solvent
- Benzalkonium Chloride
- Food Additive
- Calcium Nitrate Granules
- Phenolic Resin
- Oleic Acid
- Lauric Acid Flakes For Liquid Soap
- Maleic Acid
- Guar Gum Powder
- Borax Pentahydrate
- Monoammonium Phosphate
- Xanthum Gum
- Hardener Chemical
- Zinc Sulphate
- Zinc Chloride
- EDTA Powder
- Polyelectrolyte Powder
- Zinc Hydroxide
- Maize And Tapioca Starch
- White Dextrin
- Calcium Stearate

Plot No B 1 15, Ground Floor, Vijay Vihar, Opposite Government School Main Road, Rohini Sector 5,Delhi - 110009, India

Mr. Puneet Gupta
(Proprietor)
Mobile :08045814986
 Send Inquiry
 Send SMS

Developed and Managed by Infocom Network Private Limited.
